Índice
Introducción
CNC machining is widely used to manufacture functional plastic prototipos before an injection mold is built. A CNC prototype can help engineers evaluate product dimensions, assembly, appearance and basic mechanical performance without investing in production tooling.
However, a CNC-machined prototype is not an exact representation of a future injection molded part.
Even when both parts are described as ABS, PC, PA or another engineering plastic, differences in raw material form, manufacturing process, internal stress, geometry, surface condition and dimensional behavior can produce significantly different results.
Understanding these differences is particularly important during product development. If CNC prototype results are interpreted incorrectly, engineers may approve a design that later creates problems during injection molding—or reject a design because of a prototype issue that would not occur in production.
This article explains the practical engineering differences between CNC plastic prototypes and injection molded parts and how manufacturers should use CNC prototypes correctly before tooling.
1. The Manufacturing Principle Is Fundamentally Different
The most important difference is how the part is created.
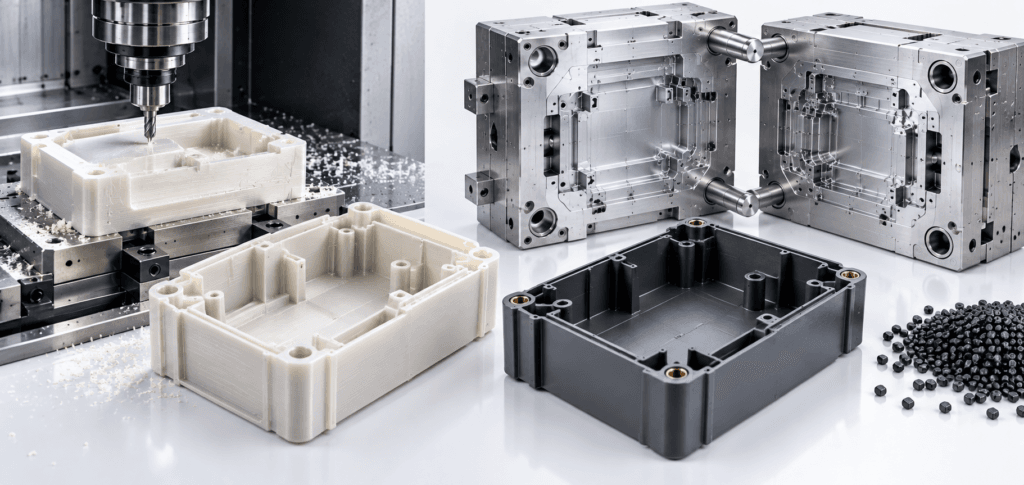
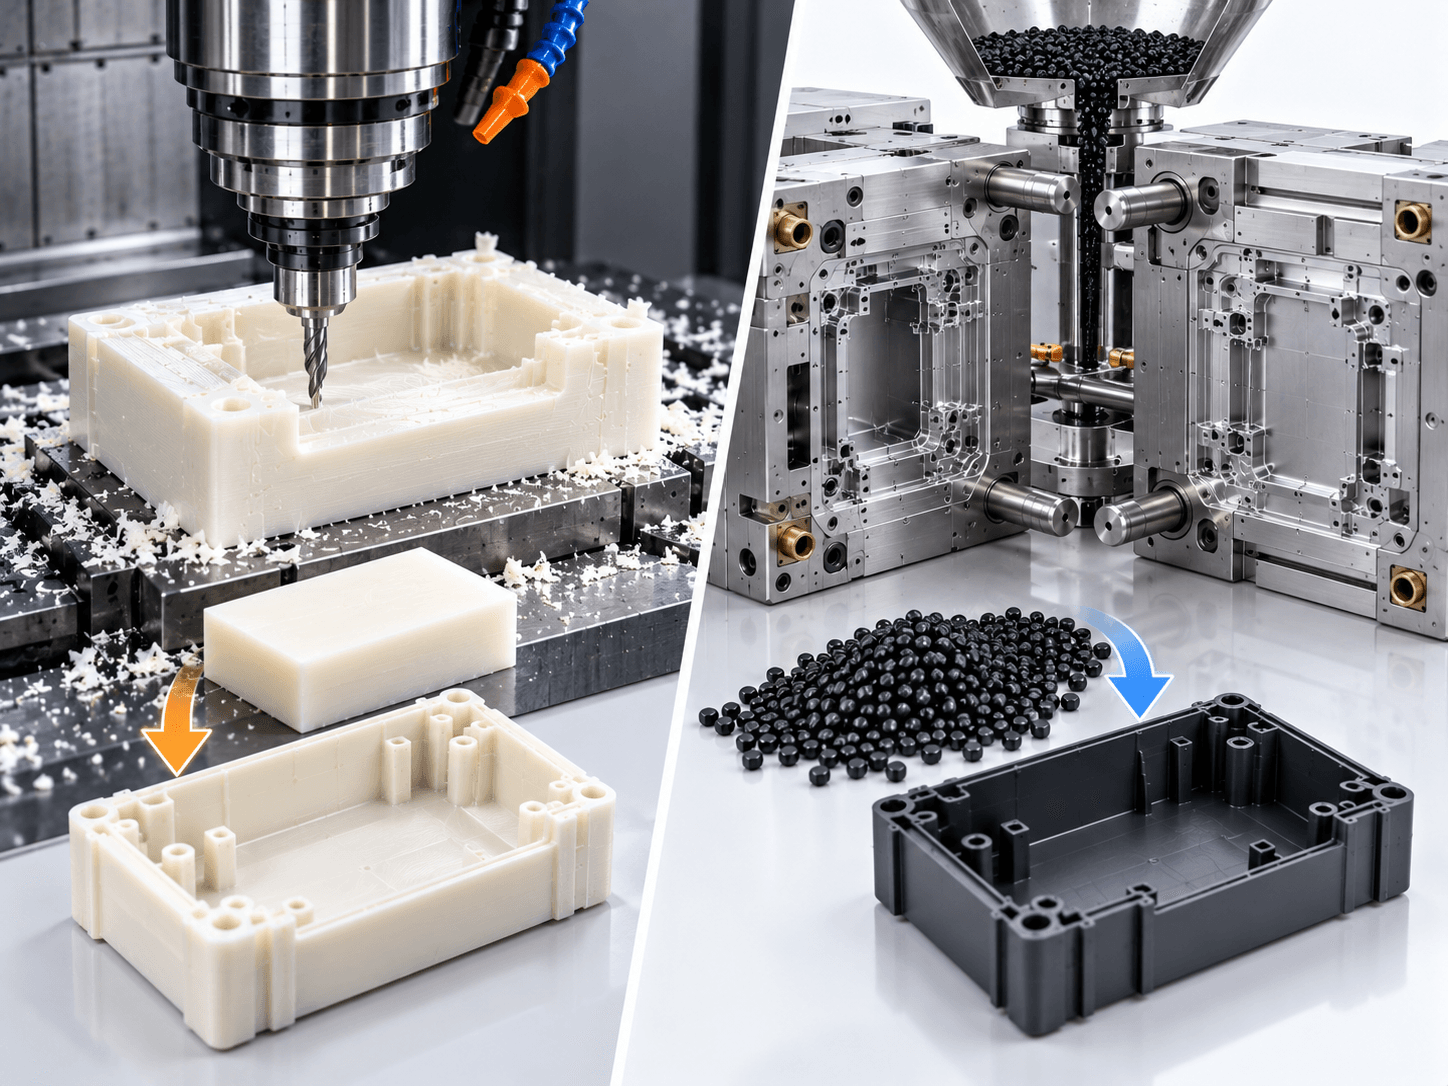
CNC machining is a subtractive manufacturing process. A plastic sheet, plate, rod or block is clamped in a machining center, and cutting tools remove material until the required geometry remains.
Injection molding works differently. Plastic pellets are melted, injected into a closed mold cavity under pressure, packed, cooled and then ejected.
Because one process removes material from a solid stock and the other forms a component from molten polymer, the finished parts do not necessarily have identical physical behavior.
| Comparison | CNC Plastic Prototype | Injection Molded Part |
|---|---|---|
| Manufacturing principle | Material removal | Melt, injection, packing and cooling |
| Initial investment | Bajo | High due to mold tooling |
| Unit cost | Relatively high | Low at production volume |
| Lead time for first parts | Short | Requires mold manufacturing |
| Design changes | Relatively easy | May require mold modification |
| Typical quantity | 1–100+ parts | Hundreds to millions |
| Main purpose | Prototype and validation | Production |
This fundamental process difference explains many of the dimensional and mechanical differences discussed below.
2. “The Same Material” May Not Mean the Same Material Performance
A common misunderstanding occurs when a CNC prototype and an injection molded component are both specified as PC, ABS or PA66.
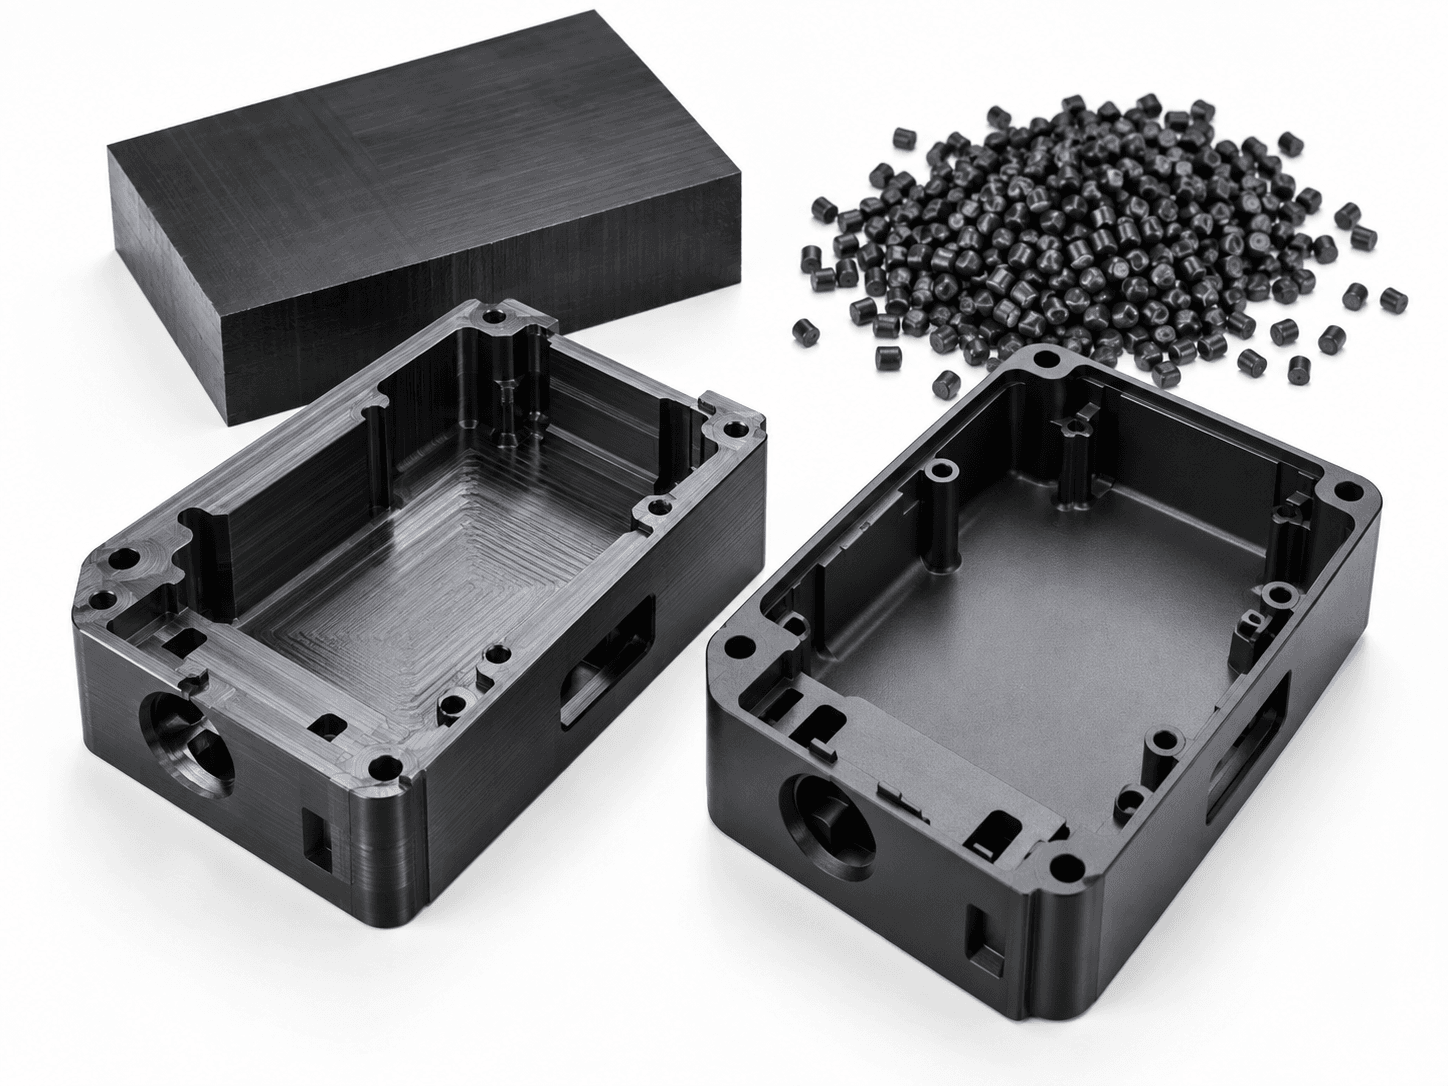
The material family may be the same, but the actual grade and material history can be different.
CNC prototypes are normally machined from commercially available plastic stock. Injection molded parts are produced from molding-grade pellets selected according to flow, impact strength, flame retardancy, UV resistance, reinforcement and other requirements.
Therefore:
CNC PC ≠ automatically the same performance as injection-grade PC.
This becomes even more important with modified engineering plastics such as:
- PC+ABS
- PA6+GF30%
- PA66+GF30%
- PA6+CF20%
- Flame-retardant PC
- UV-stabilized materials
- Impact-modified PP
When functional testing is critical, engineers should confirm whether the prototype material is sufficiently representative of the intended production resin.
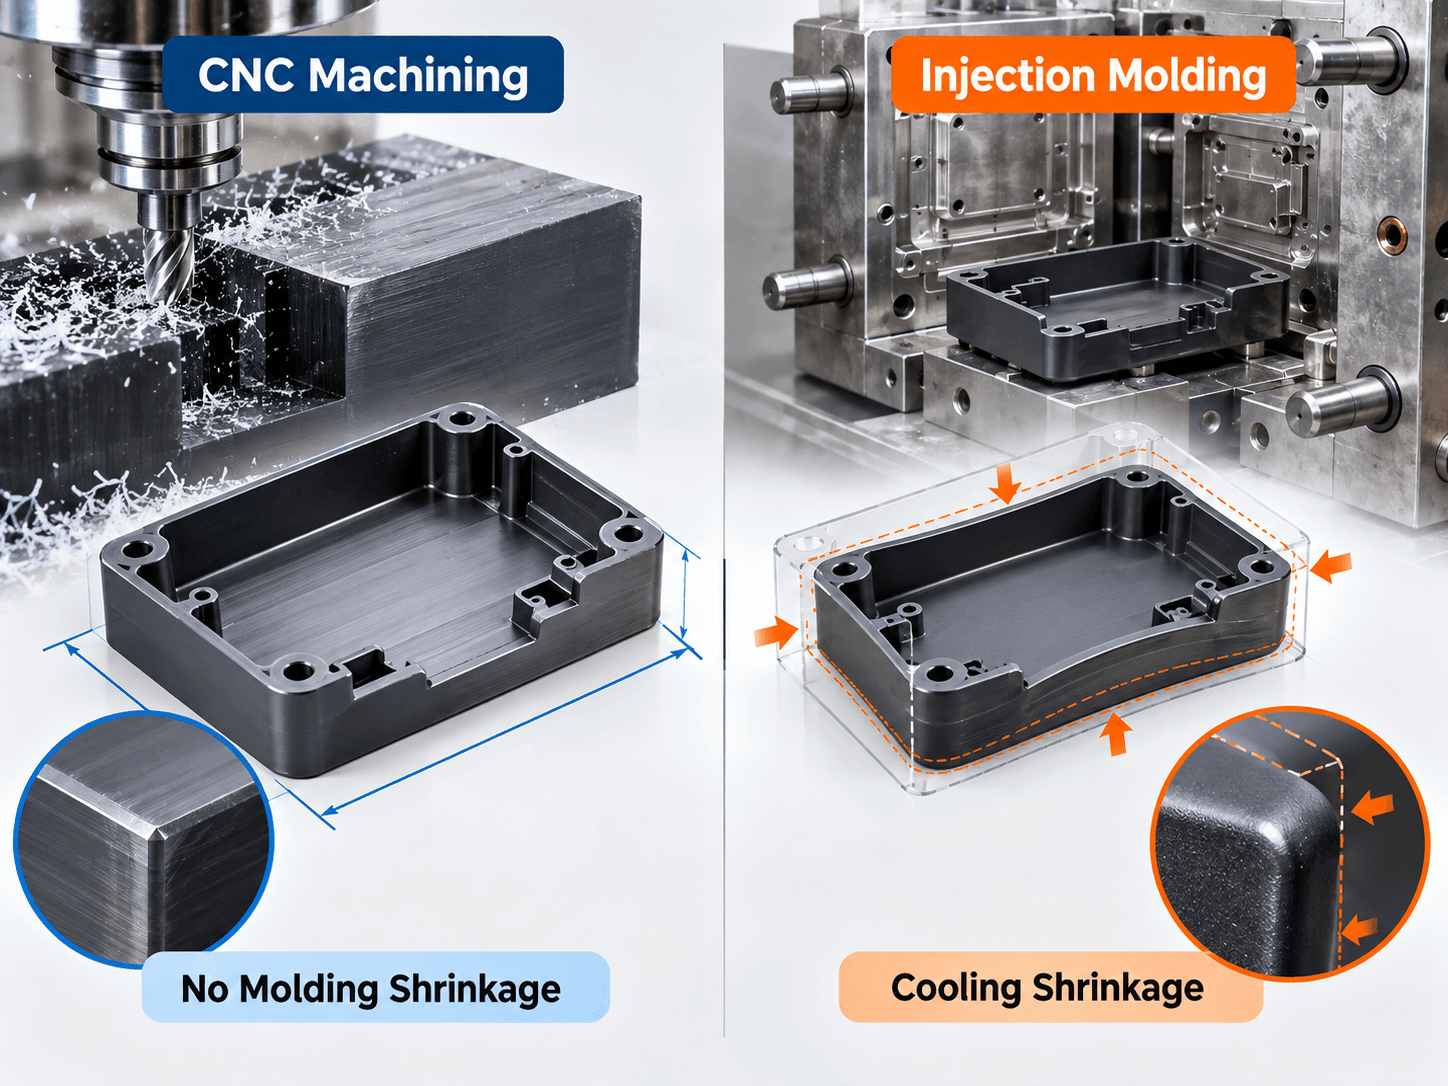
3. CNC Parts Do Not Reproduce Injection Molding Shrinkage
CNC prototypes are machined directly to dimensions from solid stock. They do not experience the same melt-to-solid shrinkage cycle as injection molded components.
Injection molded parts undergo:
melting → cavity filling → packing → cooling → shrinkage → ejection → post-molding dimensional stabilization
As a result, production parts can exhibit dimensional behavior that cannot be fully predicted from a CNC prototype.
For example, a 200 mm CNC housing may be machined very close to its CAD dimensions. A 200 mm injection molded housing, however, must account for material shrinkage, mold temperature, packing pressure, cooling conditions and geometry.
This means CNC prototypes are excellent for checking nominal assembly dimensions, but they cannot directly validate the actual molding shrinkage of a production part.
4. Warpage Behavior Can Be Completely Different
This is one of the most important differences when moving from prototype to mass production.
A CNC component is cut from a solid block. An injection molded component is formed through flowing molten polymer followed by non-uniform cooling.
The injection molding process introduces variables such as:
- Melt-flow direction
- Gate location
- Packing-pressure distribution
- Cooling differences
- Fiber orientation
- Wall-thickness variation
- Residual stress
These factors can create warpage even when the CNC prototype remains flat.
For example, a large flat enclosure might perform perfectly during CNC prototype assembly. After injection molding, the same design could show corner lifting or twisting because different areas of the component cool and shrink differently.
Therefore, a flat CNC prototype does not guarantee a flat injection molded production part.
5. Mechanical Properties Can Also Be Different
CNC prototypes are often used for functional testing, but test results must be interpreted carefully.
For unfilled engineering plastics, CNC prototypes can provide useful information about stiffness, impact resistance and assembly performance. However, their mechanical behavior may still differ from molded parts because of differences in material grade and manufacturing history.
The difference becomes more significant for fiber-reinforced materials.
During injection molding, glass or carbon fibers tend to orient according to melt flow. This can make mechanical properties directional.
A CNC-machined sample cut from reinforced stock may have a different reinforcement orientation from a molded production component.
| Prueba | CNC Prototype Reliability for Predicting Molded Part |
|---|---|
| Basic assembly | Excelente |
| Product size/ergonomics | Excelente |
| Component interference | Excelente |
| Basic structural concept | Bueno |
| Snap-fit behavior | Moderate to good |
| Exact impact performance | Requires caution |
| Molded shrinkage | Poor |
| Mold-flow-related warpage | Poor |
| Weld-line strength | Cannot be properly validated |
| Gate-related appearance | Cannot be validated |
The prototype should therefore be used to answer the correct engineering questions.
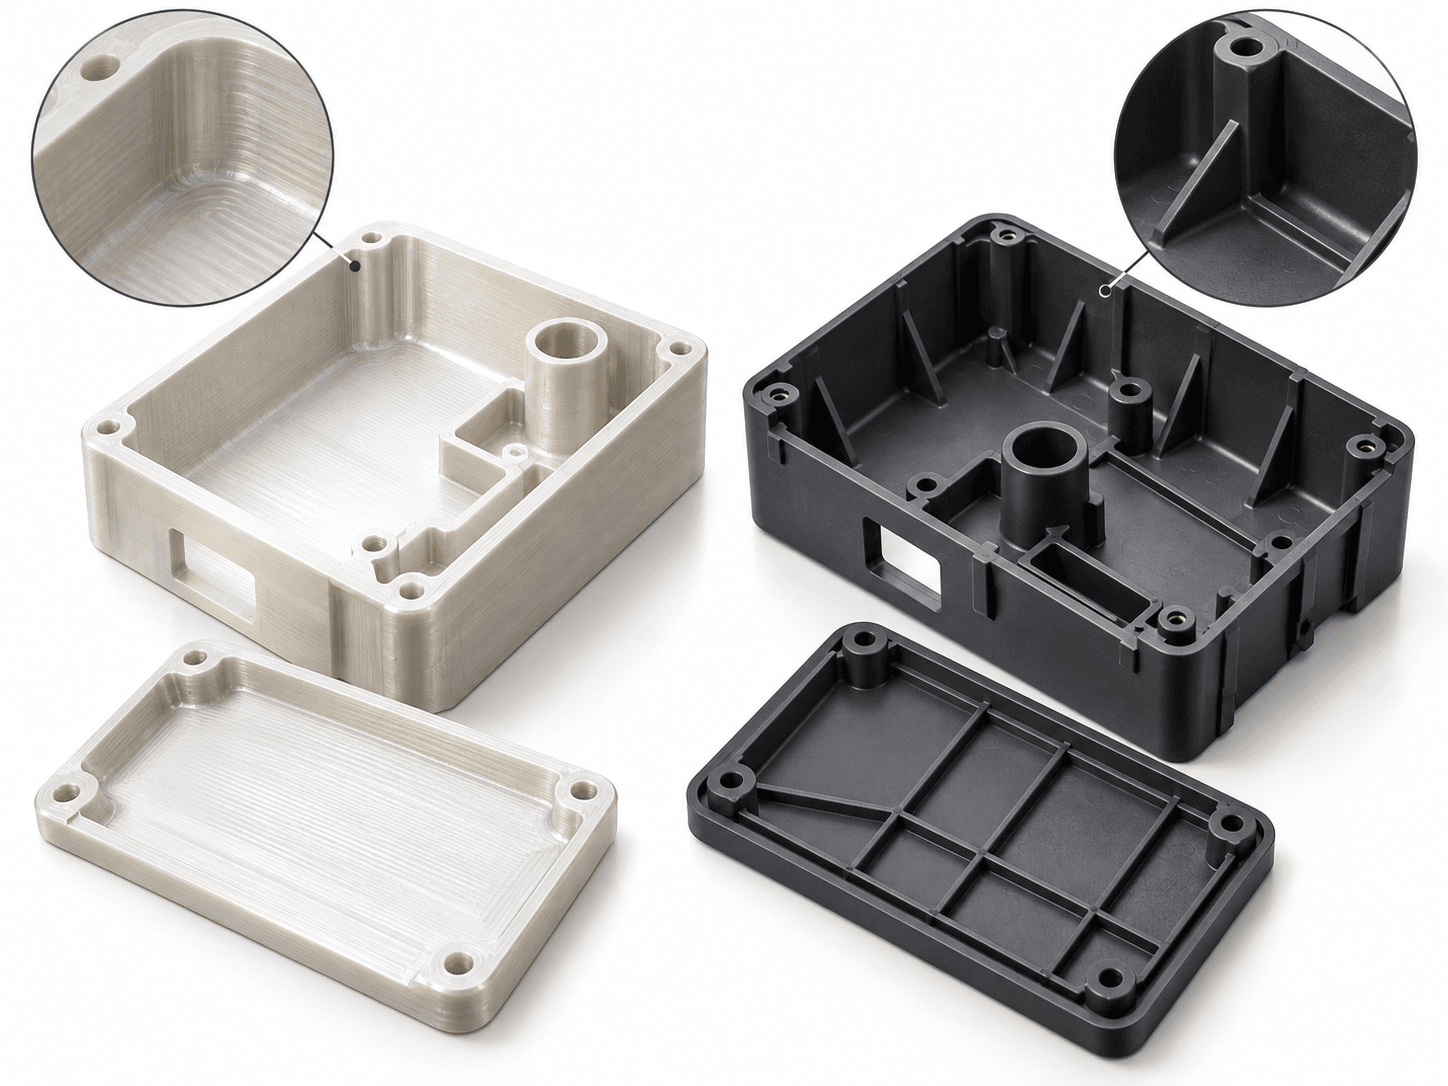
6. Some CNC Geometry Cannot Be Directly Transferred to Injection Molding
A CNC prototype can sometimes contain geometry that is easy to machine but unsuitable for injection molding.
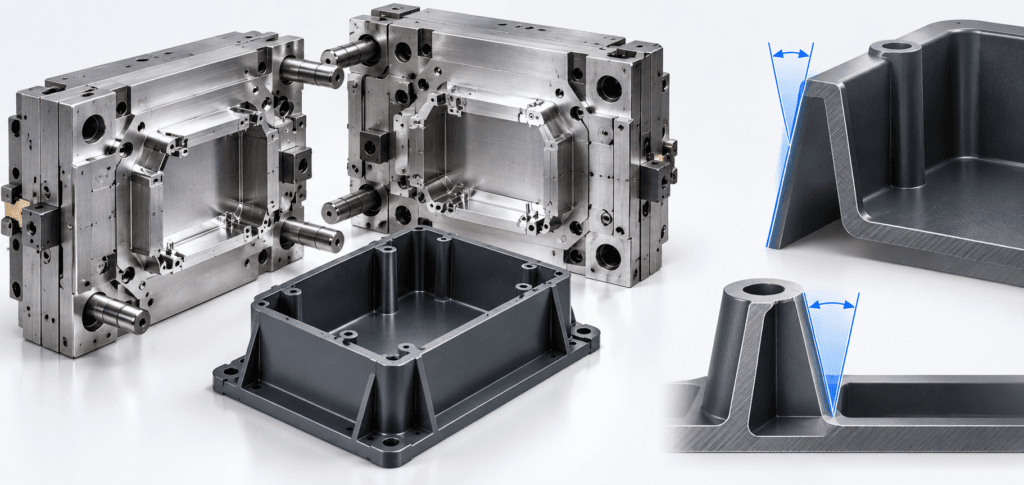
For example, a CNC-machined housing may have nearly vertical walls without draft.
An injection molded housing normally requires appropriate draft to allow reliable ejection from the mold.
Likewise, CNC machining and injection molding have different geometric constraints.
CNC-specific considerations
CNC cutting tools have physical diameters. Internal corners therefore normally contain machining radii rather than perfectly sharp corners.
Deep narrow pockets can also become difficult to machine because of tool reach and vibration.
Injection-molding considerations
Injection molded components must consider:
- Draft angle
- Espesor de pared uniforme
- Cortes undercut
- Líneas de separación
- Gate location
- Ejector locations
- Ribs and bosses
- Chupaduras
- Mold filling
- Enfriamiento
A successful CNC prototype therefore does not automatically mean the CAD model is ready for mold manufacturing.
9. Cost Behavior Changes Dramatically with Quantity
CNC machining avoids the initial cost of an injection mold, making it attractive for prototypes and low-volume requirements.
However, every CNC component consumes machine time, cutting tools and operator resources.
Injection molding requires a much larger initial tooling investment, but once the mold is validated, cycle times can be measured in seconds or minutes rather than hours of machining.
A simplified comparison looks like this:
| Project Requirement | Mecanizado CNC | Moldeo por inyección |
|---|---|---|
| 1–10 prototype parts | Highly suitable | Usually uneconomical |
| 20–100 parts | Often suitable | Depends on project |
| Design still changing | Highly suitable | High tooling risk |
| Thousands of parts | Expensive per part | Usually more economical |
| Complex molded texture | Limited representation | Highly suitable |
| Production consistency | Limited by machining process | Excellent with stable tooling/process |
The crossover quantity depends heavily on part size, complexity, material, mold specification and machining time, so there is no universal production quantity at which injection molding always becomes cheaper.
10. CNC Prototype Approval Should Not Be the Final Mold Approval
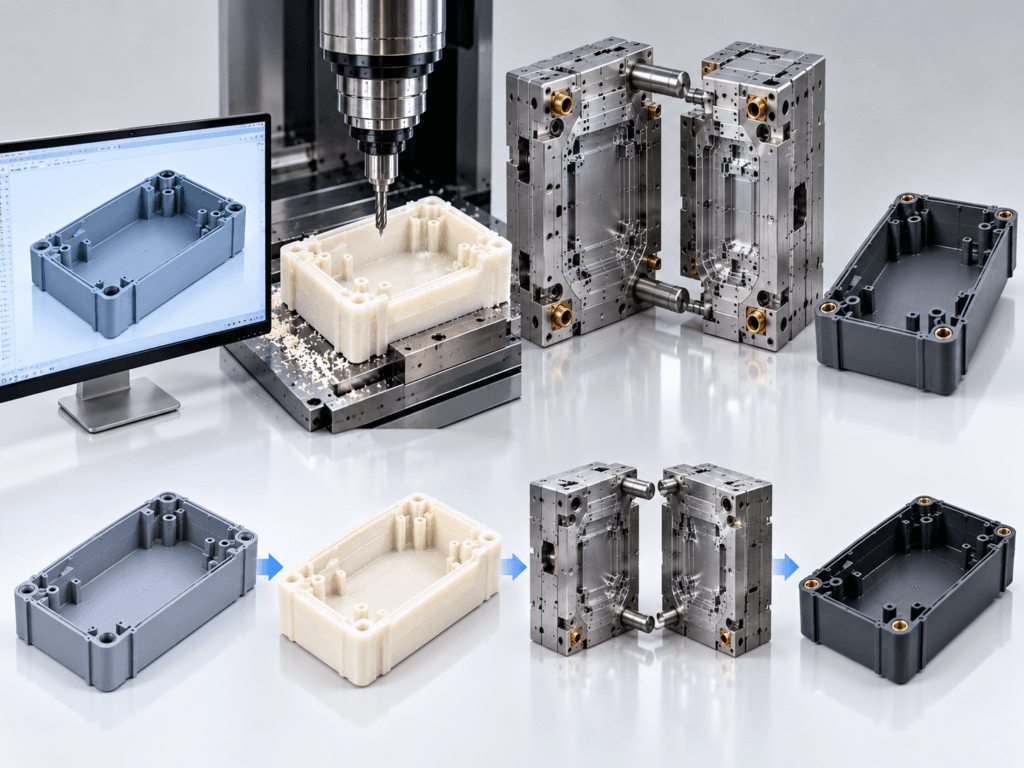
A useful product-development workflow separates prototype validation from moldability validation.
A practical sequence is:
CAD Design → CNC Prototype → Assembly Test → Design Revision → DFM → Moldflow if required → Mold Design → Tool Manufacturing → T0/T1 Trial → Dimensional Inspection → Production Validation
CNC testing answers:
Does the product design work?
DFM and mold engineering answer:
Can this design be manufactured reliably by injection molding?
T0/T1 trials finally answer:
Does the actual mold and molding process produce parts that meet the specification?
These are different engineering questions and should not be treated as interchangeable approval stages.
Conclusión
CNC plastic prototypes and injection molded parts may appear nearly identical, but they are manufactured through fundamentally different processes.
CNC machining is particularly effective for quickly validating dimensions, assembly relationships, ergonomics and basic functionality before tooling investment. However, it cannot completely reproduce injection-molding characteristics such as shrinkage, flow-induced fiber orientation, weld lines, gate marks, differential cooling, sink marks or molding-related warpage.
For this reason, CNC prototypes should not be viewed as miniature production runs. They are an engineering validation tool used to reduce uncertainty before mold manufacturing.
The most effective development strategy is to use CNC prototypes to identify product-design problems early, then perform DFM and mold engineering to convert the validated concept into an injection-moldable design.
When prototype testing and production validation are treated as separate stages, manufacturers can reduce mold modifications, shorten development cycles and achieve more predictable mass-production results.
¿Obtener el último precio? Le responderemos lo antes posible (dentro de las 12 horas)
CNC Plastic Prototypes vs. Injection Molded Parts: Key Differences Engineers Should Understand
Compare CNC plastic prototypes and injection molded parts in material properties, dimensions, warpage, surface finish, geometry, cost and production performance.
Draft Angle in Injection Mold Design: Improving Part Quality, Ejection and Tooling Efficiency
Discover how draft angles affect injection mold design, part ejection, surface texture, dimensional accuracy, ribs, bosses and long-term tooling performance.
Injection Molding Shrinkage: How to Control Part Dimensions from Mold Design to Production
Learn how injection molding shrinkage affects mold dimensions, tolerances and warpage, and how material, gate design, packing, cooling and mold trials help control final plastic part dimensions.
How to Choose the Right Injection Molding Supplier: A Practical Buyer’s Guide
Learn how to choose a reliable injection molding supplier by evaluating DFM capability, mold manufacturing, materials, quality control, production capacity, pricing, mold maintenance and technical communication.